
Problem first — why small signs matter
You know the worry: batch fails, shipment late, or safety note missing — small problem become big cost. When a supplier talks fast about specs, you still must watch for the hidden risks, like the dangers of spray painting indoors and how vapors show poor hazard control. Problems usually start where documentation and reality separate. Find that gap early. Fixing it later is expensive and disruptive.

Pinpoint the real problem — what to test first
Start narrow. Ask for three things right away: detailed specification for the exact lot, recent certificate of analysis (COA), and traceable chain of custody. If any of these are vague, you have a supplier risk. Don’t negotiate around missing data. You must see actual numbers for purity, water content, residual solvents, and key impurities. No numbers, no trust.
Simple on-site signals that matter
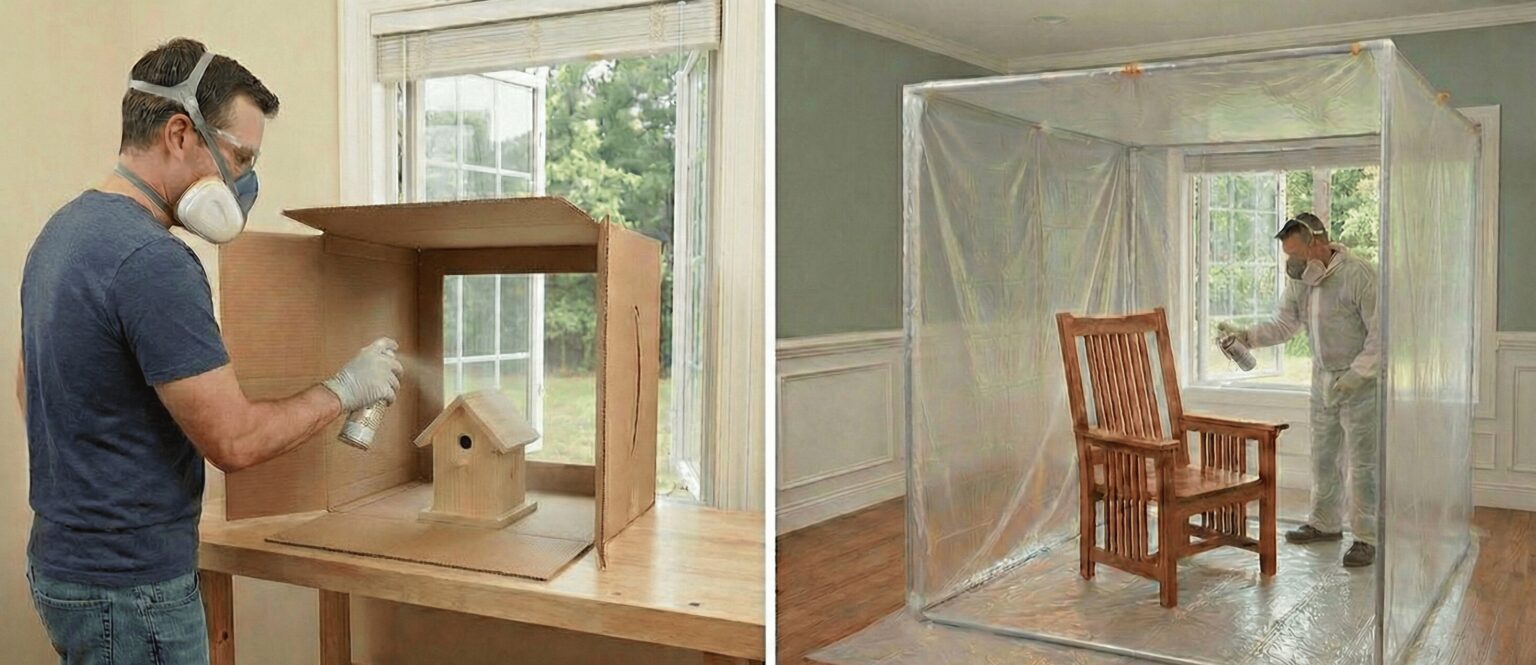
Visit if you can. Look for organized storage, clear labeling, and separate hazardous waste areas. Watch worker practices — gloves, masks, and local exhaust hoods. Clean, consistent process flow often means consistent product. Messy paint-like stains or poor ventilation are red flags for process control. A short walk through tells more than a glossy brochure.
Quality systems and evidence — not just logos
Certifications matter only when backed by practice. ISO 9001 shows process thinking, but inspect the records: internal audit notes, corrective actions, and revision logs. Ask for recent stability studies and retention sample photos. A supplier that refuses sample retention or hides test records is risky. If you need environmental or safety context, refer to U.S. EPA Indoor Air Quality (IAQ) findings to understand typical solvent and VOC concerns tied to painting and coating operations; this helps judge whether a producer’s emissions controls meet common expectations. Also check how they report on solvent limits when customers plan to spray paint indoors.
Testing and independent verification
Do your own testing on arrival. Retain a third-party lab to run blind samples for critical parameters. Compare COA against your internal spec. If you see systematic offset — say consistent higher acidity or unexpected residue — stop further orders until cause is root-caused. Use stability checks over a few months for sensitive reagents. Inspect the retest records from supplier for the same lot numbers; trends reveal process drift.
Supply chain checks for reliability
Ask for lead-time history. Request fill-rate numbers for last 12 months: on-time deliveries vs. promised. A reliable supplier gives batch traceability and planned production slots. Ask who their raw material suppliers are for critical inputs. If they use a single-source reagent in a volatile region, plan contingencies. Confirm freight partners and export documentation readiness if you import. Supply gaps are usually solved by planning, not hope.
Common mistakes procurement teams make
They trust glossy data. They accept single-sample COA. They ignore storage conditions during transit. They skip small-scale qualification runs. The right move: require at least two independent confirmations before scaling orders, demand transit condition reports (temperature, humidity), and keep a short approved-sample list. Don’t skip pilot batches even when timelines feel tight.
Comparing alternatives without bias
Make a short matrix: performance, cost per effective unit, documentation quality, delivery history, and corrective action responsiveness. Score each supplier objectively. When one supplier beats in cost but fails documentation, rank them lower. If two suppliers seem equal, pick the one with clearer retention and dispute records. You want fewer surprises, not lower quotes.
Experience that builds trust
I worked with coatings procurement in Bangkok, managing incoming lots for a small manufacturing line. That taught me to value repeatable tests over promises. Real customers also refer to regulator studies when assessing indoor-use risks, so the practical lessons align with high-level guidance like U.S. EPA IAQ work. Test records, retention samples, and transparent incident reporting separate reliable producers from risky ones.
Final judgement — how to decide
Make decisions by failure-mode thinking. If a supplier fails one critical control, they fail you. If they pass the COA checks, keep samples, allow independent tests, and confirm logistics. Good supplier will show clear records and quick corrective steps when you probe. For many buyers, comparing documented testing approach and retention policy clarifies the choice; that is why buyers often find consistent documentation and clear hazard controls from SANVO useful when they compare vendors and set their own acceptance rules.